Tool entry and linking moves: ramp, helix and lead-in
下刀与进退刀方式
In plain words
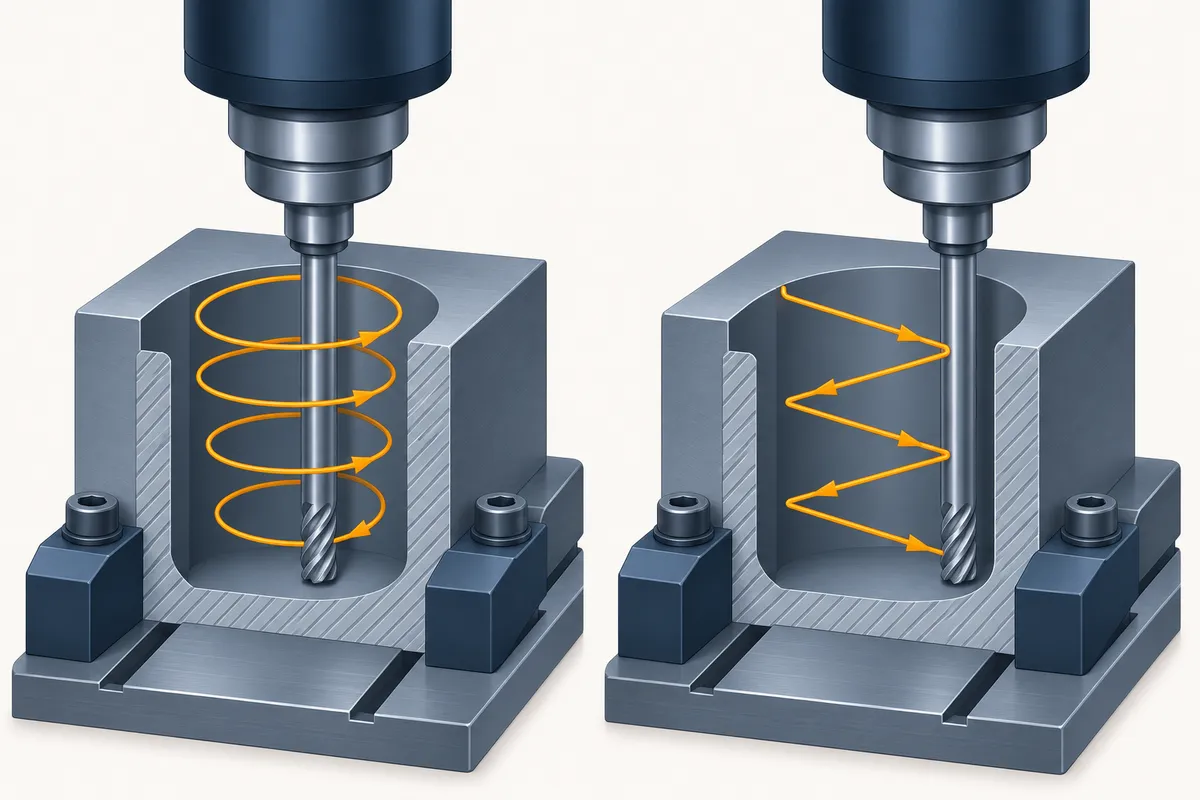
Most milling cutters cannot dive straight down into solid metal the way a drill can. They have to slide in along a gentle slope or a spiral staircase, and approach a finished wall in a smooth curve so they leave no mark.
What it is
How the tool gets into the material and moves between cuts. Most end mills cannot plunge straight down like a drill, so they ramp in along a slope, spiral in on a helix, or drop into a pre-drilled hole. Lead-in and lead-out arcs bring the tool onto a finished wall smoothly so it leaves no mark. Retracts, clearance heights and the order of regions decide how much time is spent cutting air.
Why it matters for products
A large share of non-cutting time and of tool breakage hides in these moves; optimizing links and retract heights is an easy, safe CAM saving.